Coding metal, glass and pipes
Metal, glass and pipe surfaces can look simple, but they do not all take ink the same way. The cartridge, the finish of the surface and the way the item is handled straight after coding all matter.
Hard surfaces need the right ink behaviour
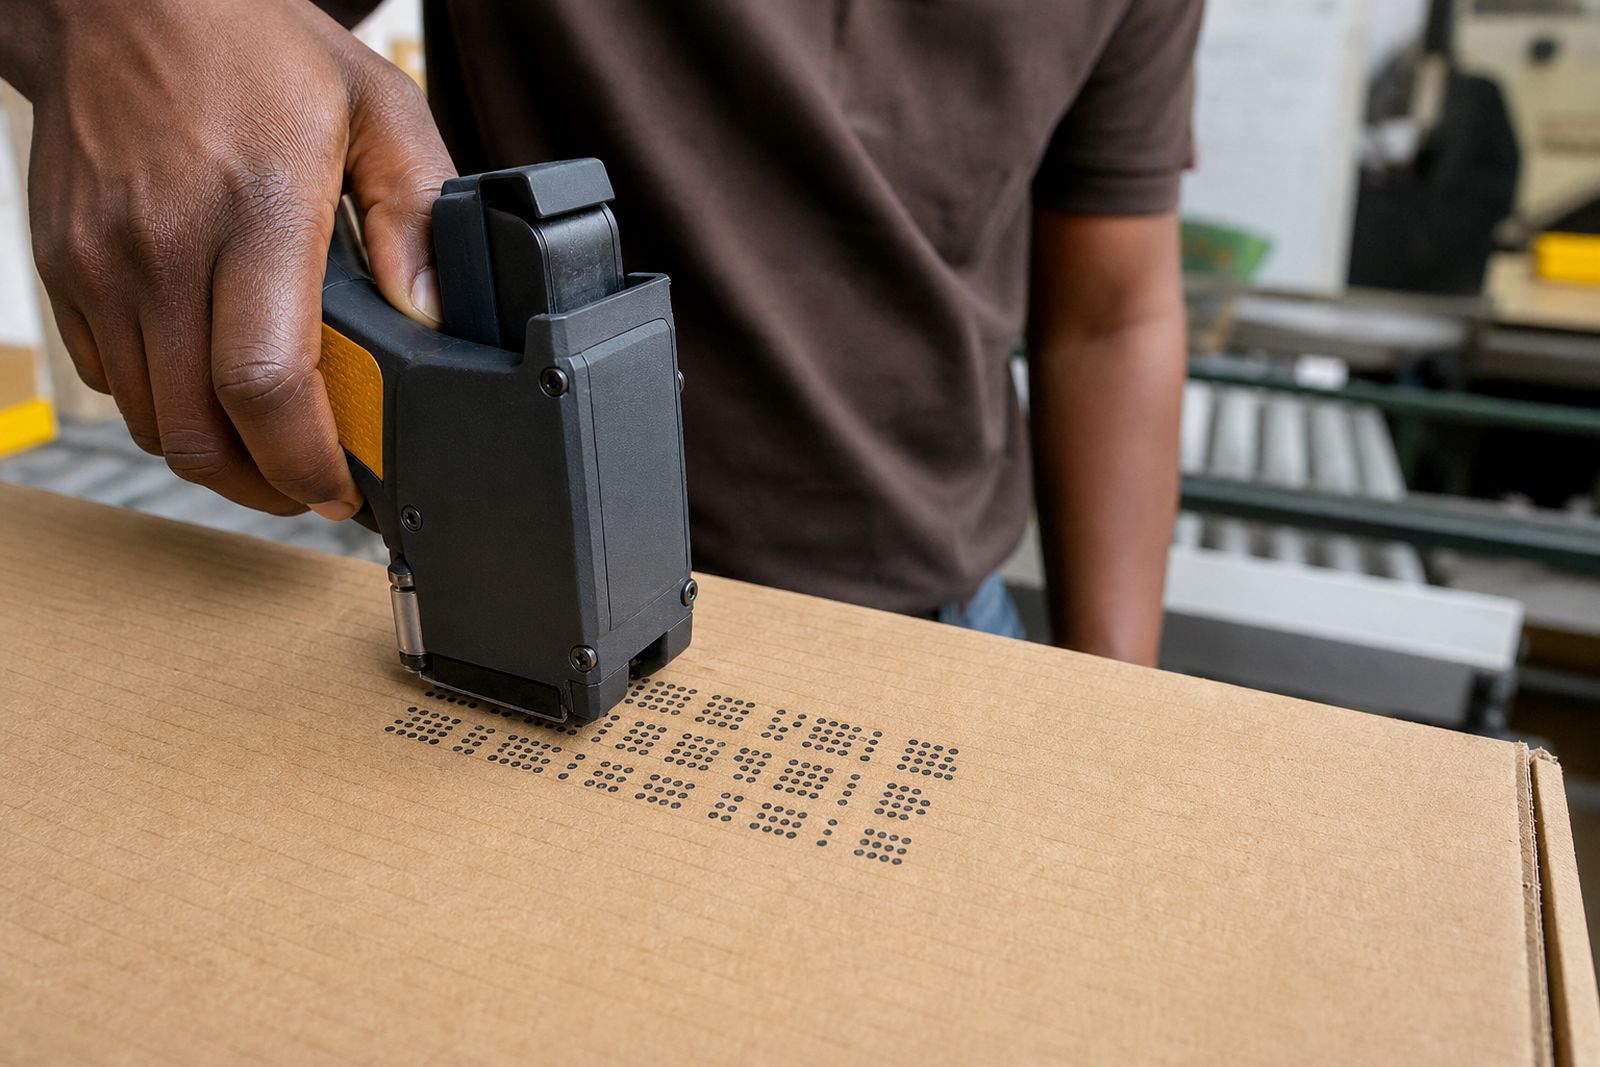
On cartons and raw timber, ink can soak in slightly and hold a mark in place. On glass, coated metal and many plastic-lined cans, there is nowhere for the ink to go, so the code must dry on the surface itself. That is why smooth hard items usually need a quick-dry solvent cartridge rather than a water-based one.
The surface finish matters as much as the material. Bright tin, powder-coated tube, oily extrusions and cold glass jars can all behave differently under the same coder. A mark that looks dark and clean on one batch may wipe or feather on the next if the finish has changed, or if condensation is present. In South African coastal conditions around Durban and Pinetown, that catches people out quite often.
- Glossy and non-porous surfaces usually need fast-evaporating solvent ink.
- Cold containers can attract moisture which interferes with adhesion.
- Protective oils on metal stock can weaken the code if the area is not clean.
- Dark pipe and coated steel often need white or coloured ink for contrast.
Cans and jars on packing lines
Cans and jars are handled quickly, often while labels, lids and date coding are all happening in the same work area. The usual problem is not getting the code onto the item, it is keeping the code legible after the container rolls, touches guides or is packed into outers. A quick-dry cartridge helps, but print position is just as important.
On jars, many teams place the code on the shoulder, lid edge or a clear area of the glass where scuffing is lower. On cans, a flatter part of the body or end panel tends to give a steadier mark than a curved seam area. If the item is chilled before coding, wait until the condensation issue is understood, otherwise the print can break up or rub off even when the cartridge choice is broadly right.
Where a line handles both jars and cartons, it is worth separating cartridge use by surface rather than trying to force one ink across everything. It sounds convenient, but mixed substrates usually punish that shortcut later.
Pipe lengths and extrusions in the workshop
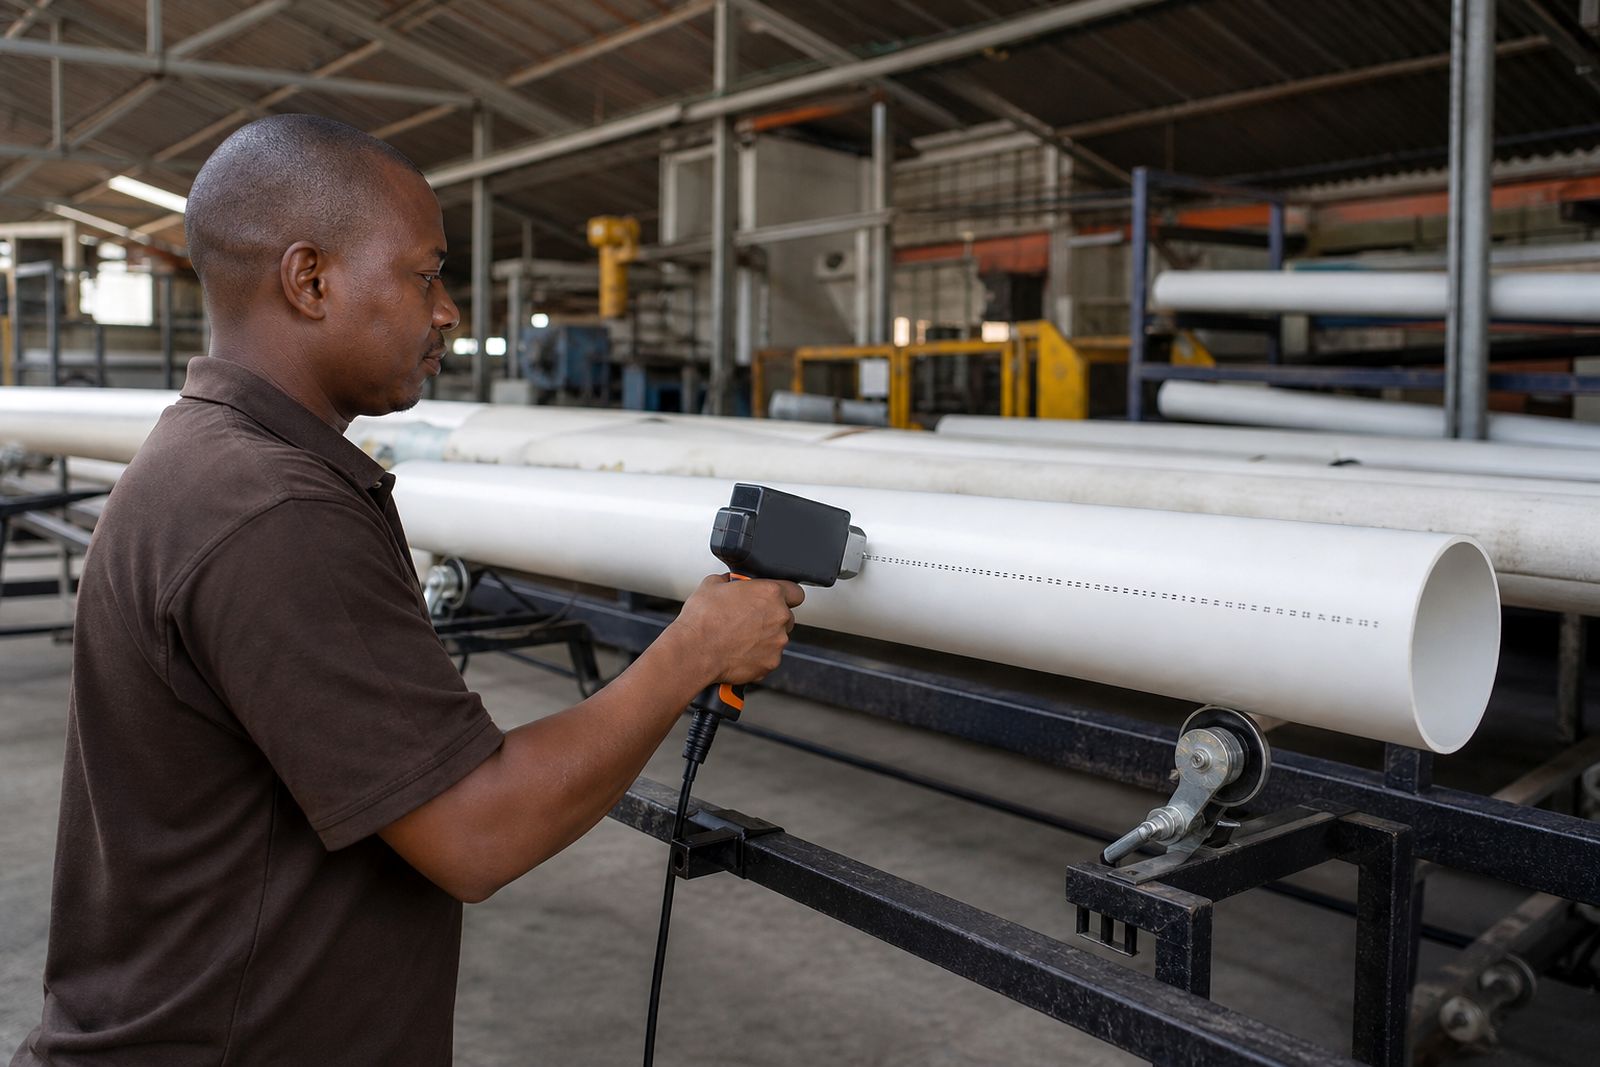
Pipe, conduit and metal extrusion work has its own pattern. The item is long, the coding area may move past the operator, and the message often needs to stay readable after stacking, loading and site handling. Batch details, size marks and job references must remain clear even when the pipe has a dark finish or a slight curve.
A workshop in Pinetown recently had this exact issue on black pipe lengths going out to sites inland and along the coast. The team could get a code onto the pipe, but on some lengths the mark looked grey and thin. The real cause was a combination of surface colour, slight residue from handling and the print height being set a bit too far off the pipe. Once they moved to a higher-contrast cartridge and tightened the print distance, the code looked more even. They also kept the coding area cleaner between batches which helped more than expected.
- Keep the print gap consistent along the pipe or extrusion.
- Check for handling residue, dust and cutting fluid near the code area.
- Use white or coloured ink where black marks disappear into the surface.
- Test the code after stacking, not only straight off the line.
When white or coloured inks make sense
Contrast is often the difference between a code that passes inspection and one that creates rework. On silver metal, standard dark ink may be enough. On black pipe, blue drum lids or coated components, a white or coloured cartridge can be the better choice because the mark reads from farther away and under mixed factory lighting.
That said, contrast alone does not solve every problem. A bright white code still needs the correct cartridge chemistry for the surface, and the nozzle has to stay clean. If a line runs only occasionally, dried residue at the print head can spoil character edges and make numbers look incomplete. Regular nozzle care matters most with high-contrast jobs because every flaw shows.
For export cartons packed with metal parts, some teams use one cartridge for the carton and another for the coded part inside. That is normal. The substrate decides the ink, not the convenience of keeping only one cartridge on the shelf.
Small checks before a full production run
A short test on the real item saves cartons, labels and labour. Metal and glass jobs should be checked not only for legibility but also for handling resistance. If the item is washed, shrink-wrapped, packed while still cold or moved through dusty areas, those conditions need to be part of the test.
- Print on the actual finished surface, not a sample offcut from another batch.
- Rub the code only after it has had a fair chance to set.
- Check the mark after packing contact, not only as a fresh print.
- Look at the code under the lighting used by operators and dispatch staff.
- Keep a sample from each batch while you compare cartridge performance.
If the code looks faded, the cause may be poor contrast, too much print distance or a nozzle issue rather than the wrong message settings. If the mark smudges, look at the surface condition first. We help customers match cartridges to the coder and substrate, and our contact form is the best place to send a brief note on the material you are coding.
Storage and handling matter more than people think
Cartridges for hard non-porous surfaces need sensible storage and careful fitting. Leave caps off too long, store cartridges in heat or let dust build up around the nozzle area, and print quality usually drifts before anyone notices. In busy warehouses that code pipes, drums and glass containers in the same week this is common, especially when spare cartridges move between benches.
Keep cartridges sealed until needed, store them in stable conditions and wipe the print area using the handling method recommended for that cartridge type. The goal is a clean nozzle and a consistent mark, not endless adjustment on the coder. We do not sell or repair the coders themselves, but we do help customers choose the right cartridge for metal, glass and pipe applications and courier orders to factories, packhouses and warehouses across South Africa.
What our Coding Ink customers say
Verified Google reviews
Questions we get asked
Can one cartridge cover metal, glass and cartons?
Usually not well. Cartons and paper often suit water-based ink, while smooth non-porous items like metal and glass normally need a quick-dry solvent cartridge.
What causes a code to wipe off a glass jar?
Common causes include condensation, an unsuitable cartridge, a dirty surface or handling the jar too soon after coding. The finish of the glass can also affect adhesion.
Do dark pipes need a special cartridge?
They often need higher-contrast ink such as white or another visible colour, matched to the surface and to the handheld coder being used.
Tell us about the job
Send sizes, materials and where you are through our contact form, and we will come back with the practical options.
Open the contact form